Genesis Medical Plastics converts implantable PEEK and other high performance medical polymers into prototype and low volume components at an ISO 13485:2016 and ISO 9001:2015 certified, FDA registered site in Cypress, Texas. Prototypes run on the same validated processes as production, which is the point: a geometry proven at prototype does not have to be requalified to scale.
Which Conversion Routes Are Available for Prototypes?
Genesis runs four conversion processes in one plant, and a prototype can come from any of them:
Injection molding, where the prototype has to represent a molded production part.
Prototypes run on the same validated processes as production parts.
What Are the Benefits of Each Conversion Route?
Machining from stock is the fastest route to a physical part and the most forgiving of design change. No tooling, so a revision costs a program file rather than a mold. It is the right route for form and fit evaluation and for early functional testing.
Injection molding is slower and more expensive to start because it needs tooling, but it is the only route that produces a part with production molding’s thermal history, crystallinity and internal stress. If the production part will be molded, a machined prototype will not tell you everything the molded part will do.
Extrusion matters when the prototype’s properties depend on the stock form itself rather than on the finishing.
Calendering is the route for anything requiring film, which cannot be usefully approximated by machining a thin section from plate.
The practical sequence for most programs is machined prototypes for form, fit and early function, then molded prototypes from production intent tooling before design freeze if the production part is molded.
Can Prototypes and Production Parts Be Made From the Same Grade of Polymer?
Why the question matters more than its volume suggests: the largest avoidable risk in a prototype program is qualifying a part in one material and discovering at scale that production needs a different grade, a different form, or a different supplier. That is a requalification, and on an implantable program it is expensive in both money and calendar time.
Where the same grade carries from prototype through production, converted on the same validated processes at the same site, that risk is designed out at the start rather than managed later.
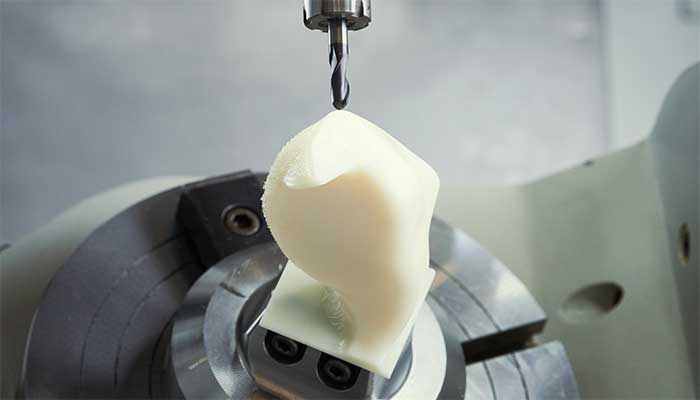
Machining from stock is the fastest route to a physical part and takes no tooling.
How Does a Prototype Move to Production?
The transition is mostly a documentation and validation question rather than a manufacturing one, provided the prototype was made on validated processes to begin with.
Same material, same documentation chain. If the prototype used implantable grade stock with traceability, the material half of the qualification is already established.
Same conversion processes, already validated. Genesis conversion processes carry IQ, OQ and PQ. Volume changes; the validated process does not.
Same quality system. ISO 13485:2016 and ISO 9001:2015 apply at prototype quantity as at production quantity.
One supplier across the transition, so scaling does not introduce a new material source or a new quality system at the point of greatest schedule pressure.
Molding needs tooling, but it is the only route that reproduces a molded part's thermal history.
What Does Genesis Need to Quote a Prototype?
A drawing or a 3D model with tolerances.
The material, or the requirement if the material is not yet chosen.
Quantity, and whether production volume is known.
Whether the component is implantable, since that determines the grade and the documentation.
Any sterilization requirement.
Genesis does not publish lead times.
Low volume production on the same equipment that made the prototype.
Prototype Capabilities
Genesis converts implantable PEEK, PEEK film, ZFUZE Therapeutic Biomaterial and a range of sulfone and high performance grades including Radel PPSU, Udel PSU, Eviva PSU, Veriva PPSU and Ultem, across four conversion processes in one plant. Quality system ISO 13485:2016 and ISO 9001:2015, FDA registered site, IQ, OQ and PQ validated processes, ASTM F2026 compliant PEEK stock.
What Does a Prototype Have to Prove?
A prototype is not a smaller production part. It is an instrument for answering a specific question, and the question determines the route.
Form and fit prototypes answer whether the geometry works in the assembly. They can be machined from any reasonable grade, quickly, because nobody is measuring material behavior yet.
Functional prototypes answer whether the material survives the duty cycle. These have to be made from the production grade, because a part machined from a substitute will give a confident and wrong answer about stiffness, creep or sterilization tolerance.
Production intent prototypes answer whether the manufacturing process holds the drawing at volume. These have to be made by the production route, which is why a molded part cannot be validated by machining one.
Programs that skip the middle category are the ones that discover a material problem during design verification, which is the most expensive place to find it.
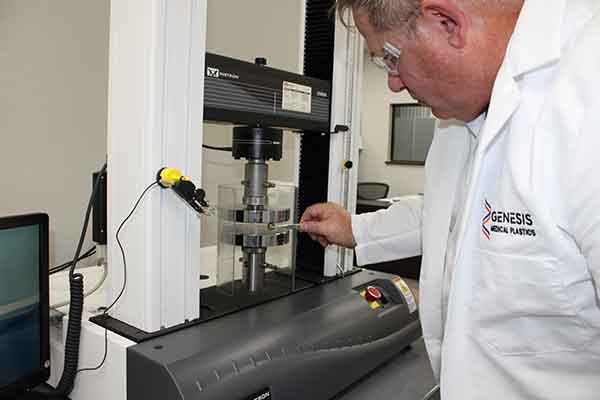
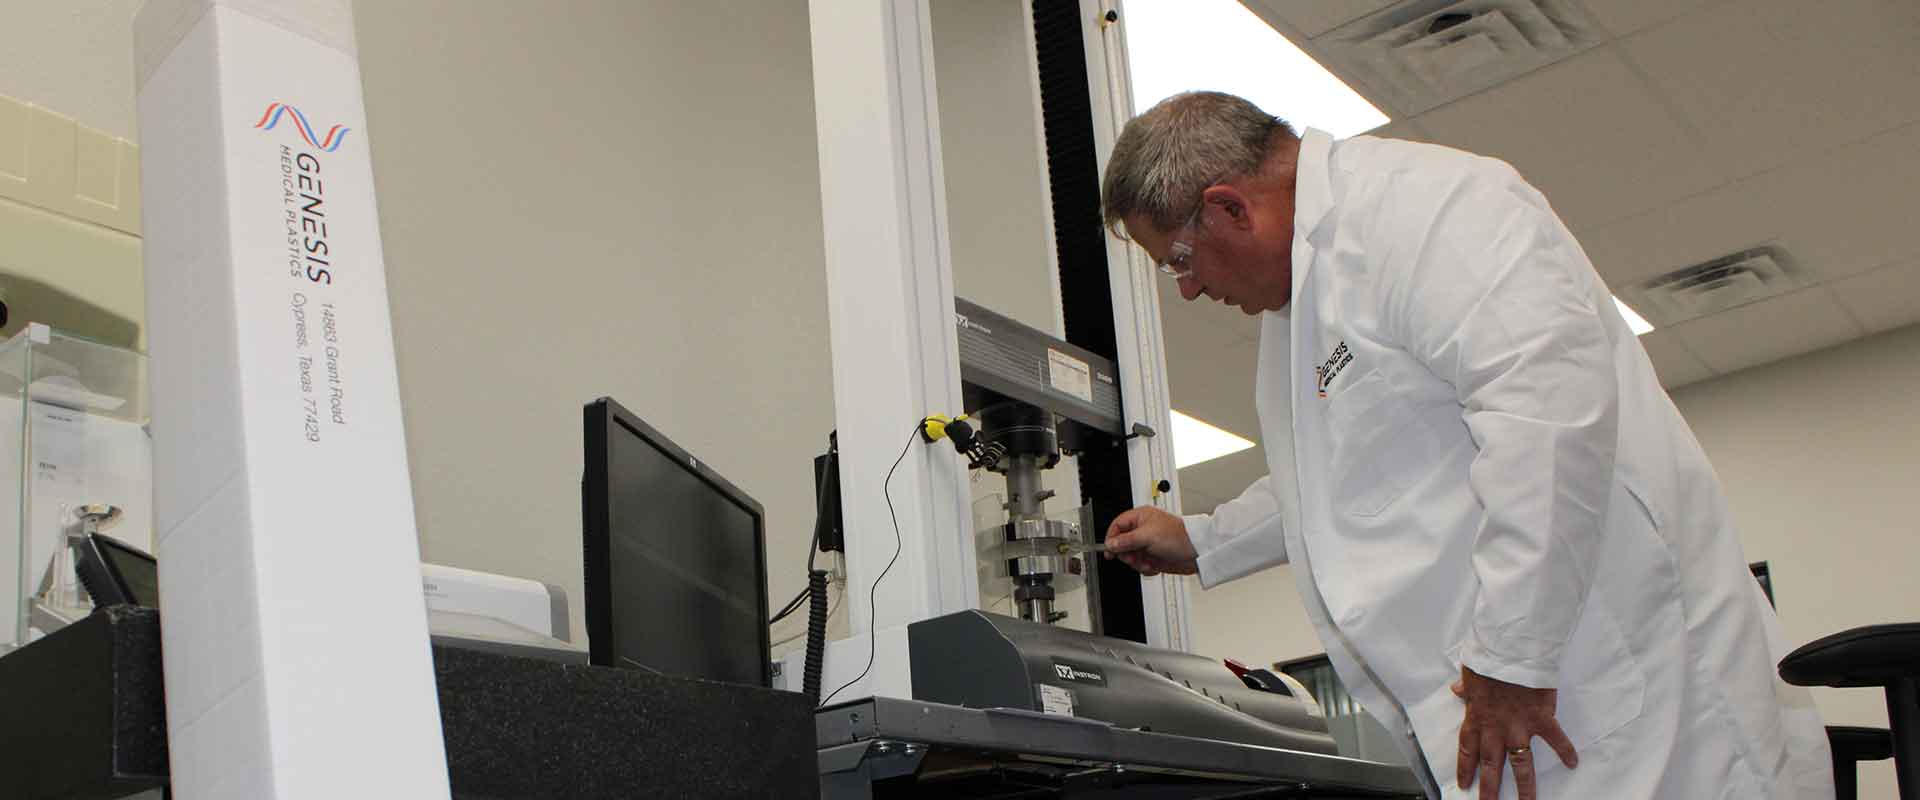
Laboratory testing conducted in Genesis’ lab confirms physical properties of medical polymer formulations.
How Do Prototype Tolerances Differ From Production?
They usually should not. A prototype held to looser tolerances than production tells you the design works when it is made well, which is not the question production has to answer.
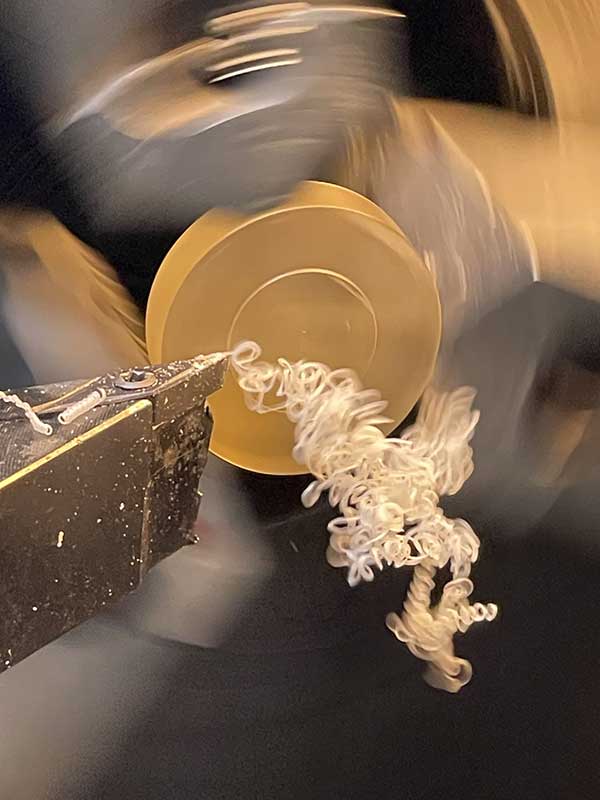
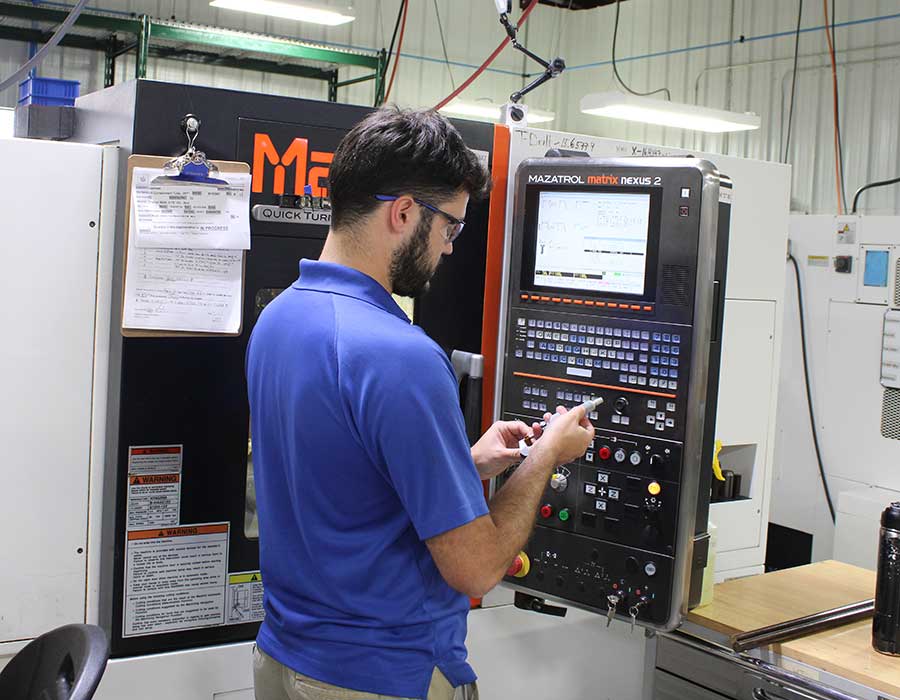
Genesis machines prototypes on the same equipment and the same validated processes as production components.
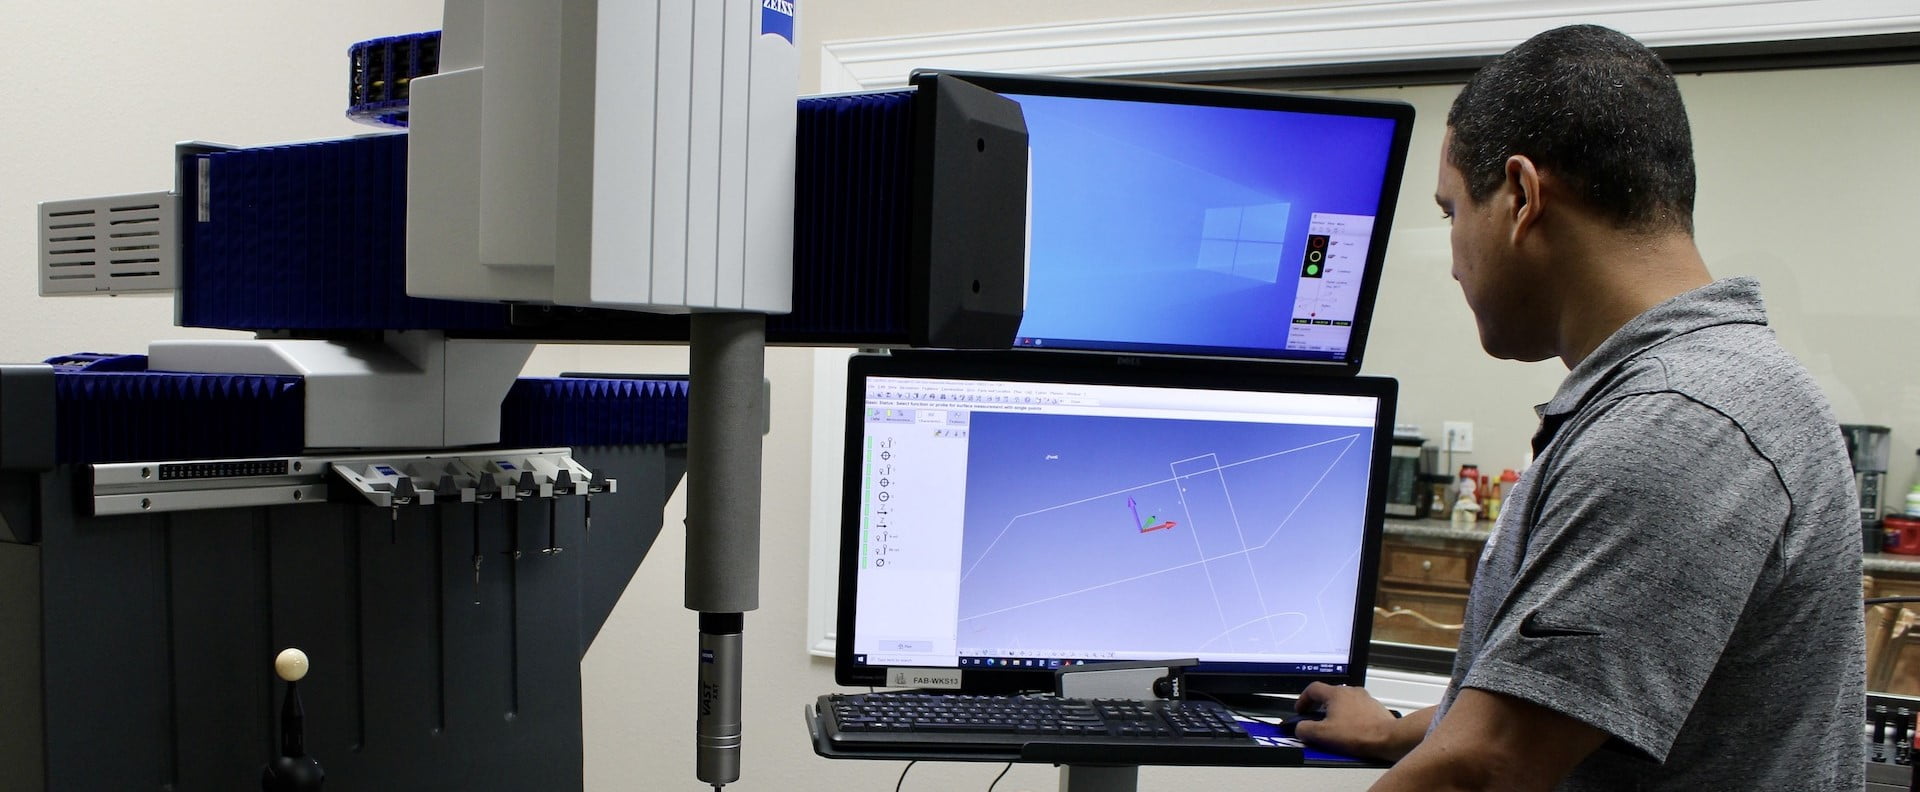
Best-in-class machining technology in Genesis’ facility produces precision prototypes and production quantities of medical device components.
What Changes When a Prototype Uses Implantable Grade Material?
Everything about the documentation, and nothing about the geometry.
Implantable grade stock carries traceability to the resin lot and compliance to the relevant material standard, ASTM F2026 in the case of PEEK stock for surgical implants. A prototype made from that stock can support a design history file. A prototype made from an industrial grade of nominally the same polymer cannot, no matter how well it is machined.
This is the single most common avoidable error in early stage implantable programs: prototyping in an industrial grade because it was available, then discovering the test data cannot be used.
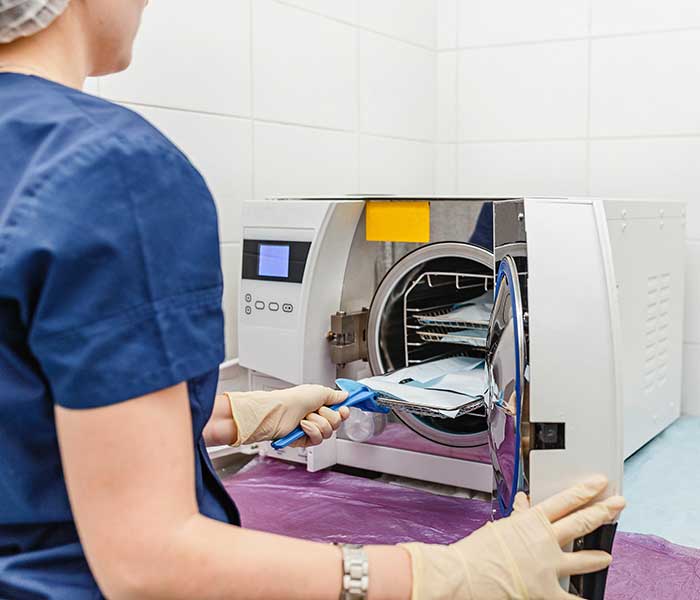
Prototypes can be tested to verify a medical polymer’s performance and the component’s design under actual conditions such as repeated autoclaving.
What Are the Common Reasons a Prototype Program Stalls?
Four, in rough order of frequency. The drawing has no tolerances, so there is nothing to inspect against. The material is named by tradename only, without a grade, so the wrong variant gets quoted. The sterilization requirement arrives after the material is chosen. And the volume expectation is unstated, so a part gets machined that should have been molded, or tooled that should have been machined.
All four are cheap to fix before quoting and expensive to fix after.
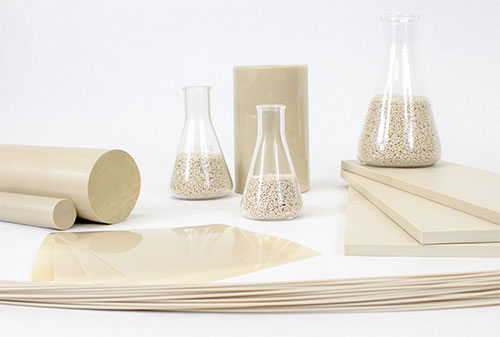
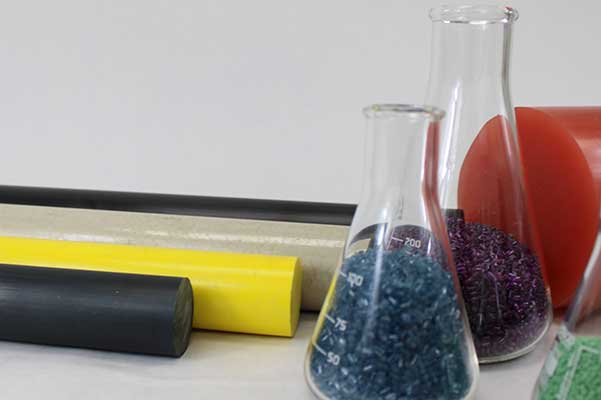
Genesis extrudes customers’ many different medical polymer formulations into custom size rods and plates for machining into prototypes as well as production parts.
Stages of Medical Device Prototyping
Medical device prototyping moves through stages. Each one answers a different question for the engineering team, and the right material and conversion route change as the device design matures.
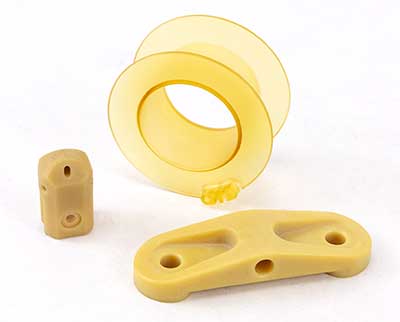
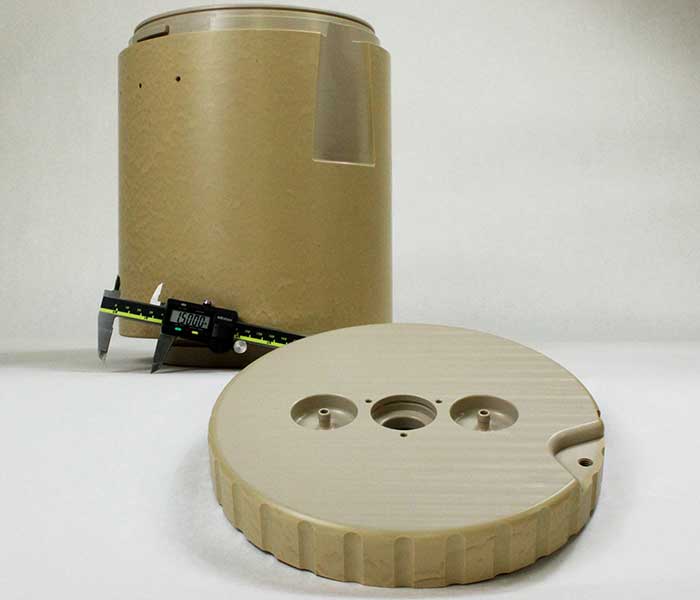
PEEK prototype components.
Concept and Proof of Concept Models
Early models test the idea itself: does the mechanism work, and does the device fit the anatomy and the procedure? Speed and low cost per iteration matter most here, so machining from stock is the usual route.
Iteration and Design Feedback
Designers, engineers and clinicians test successive versions for functionality and usability, and feed the results back into the design. Each iteration should change one thing deliberately, so the feedback is clear.
Design Verification and Validation Builds
Parts for verification testing have to represent the production device in material, process and documentation. This is where production grade material and validated conversion processes stop being optional.
Pilot and Pre Production Builds
Final builds confirm the manufacturing process holds the drawing at volume, and they produce the parts used in the later stages of the approval pathway.
How Prototyping Fits Design Controls and Regulation
FDA design controls, now aligned with ISO 13485 under the Quality Management System Regulation, expect a device developer to document how design inputs become outputs, and how the design is verified and validated. Prototypes are evidence in that record.
Machined prototype components from medical grade stock.
Why Material Traceability Matters Early
Test data from a prototype only supports the design history file if the prototype’s material and process are documented. Building prototypes from traceable, medical grade stock under a certified quality system keeps that data usable.
Controlling Development Costs
The most expensive prototyping mistake is one discovered late, such as a material change after verification testing. Choosing the production grade and a converter that runs all four conversion routes early keeps development costs and timelines predictable. See the full list of medical polymers Genesis converts.
Request a Quote for a Prototype
Send a drawing and Genesis will quote the conversion route that fits the stage the program is at. Request a Quote, or Contact Our Experts. Call 281-255-6848.
Can Genesis make prototypes from implantable grade material?
Yes. Prototypes are converted from the same implantable grade stock, on the same IQ, OQ and PQ validated processes, under the same ISO 13485:2016 quality system as production components.
Should a prototype be machined or molded?
Machining is faster and takes no tooling, which suits form, fit and early functional evaluation. Molding requires tooling but is the only route that reproduces a molded production part's thermal history and internal stress. Programs headed for molded production usually do both, in that order.
What information does Genesis need to quote?
A drawing or model with tolerances, the material or the requirement, quantity, whether the component is implantable, and any sterilization requirement.