Genesis injection molds medical device components from implantable PEEK and other high performance medical thermoplastics, using all electric machines and documented process control under an ISO 13485:2016 quality system. The medical plastics specialist injection molds implantable and proprietary polymers its customers specify, or supply for toll conversion, and many of the medical grades it converts into its extruded shapes and machined parts. As a result, a component can move from the prototype stage to production parts machined from stock shapes to injection molded parts without changing supplier.
Materials Genesis converts
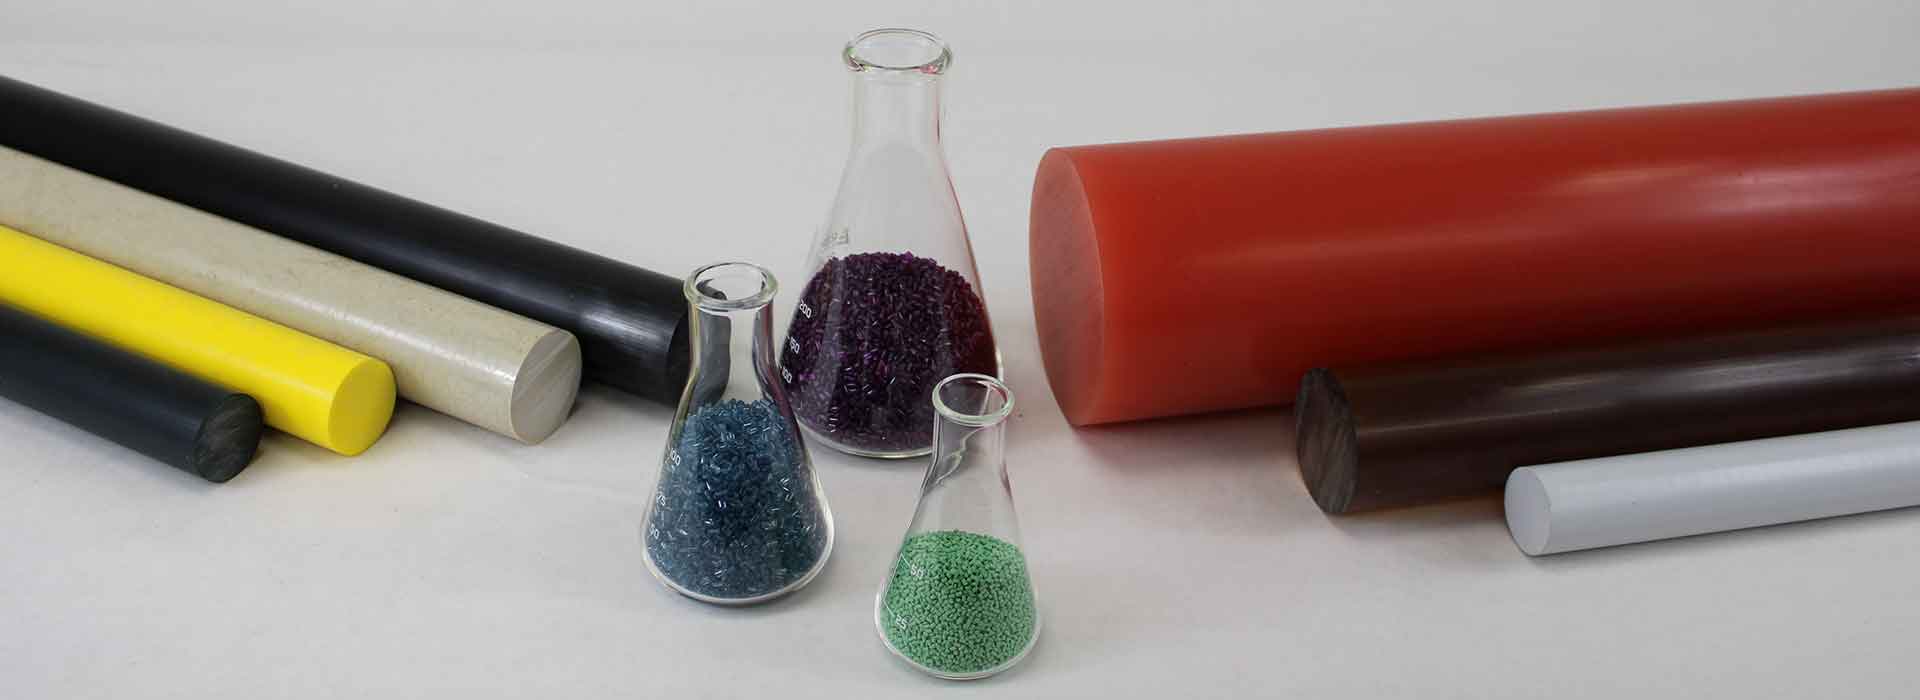
Genesis converts a comprehensive range of implantable polymers and medical grade plastics into injection molded parts, extruded shapes and machined components.
Implantable Genesis PEEK
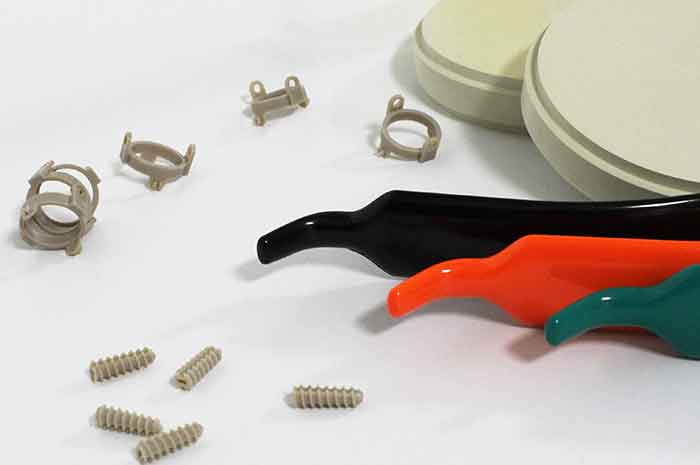
Genesis injection molds and extrudes implantable PEEK resins specified by its MDM customers or supplied by them for toll manufacturing.
The company also converts its Genesis PEEK resin into extruded shapes and machined parts, and into injection molded components. The benefit of this vertical manufacturing approach for MDMs is that a device’s traceability and process history stay under one quality system through a device’s life cycle. See Genesis PEEK.
Implantable PSU and PPSU
Syensqo’s Veriva PPSU (polyphenylsulfone) and Eviva PSU (polysulfone) are also available from Genesis as injection molded parts and extruded shapes. The sulfone polymers are similar in performance to their medical grade counterparts, Radel PPSU and Udel PSU, and also available in transparent tints. See Eviva PSU and Veriva PPSU.
Medical plastics
Genesis injection molds the medical plastics from which it extrudes its stock shapes for machining. Where differences such as melt viscosities exist between a molding and extrusion grade, Genesis has a history of working with customers when necessary to develop process conditions and adapt equipment so the same polymer grade can be converted by both methods.
The list of medical plastics Genesis converts by injection molding and extrusion, and their main attributes, includes these major healthcare polymers:
- PEEK (polyetheretherketone) has a long history in medical device applications and instruments that precedes its long-term implantable counterparts. Its notable properties include high strength and temperature resistance, compatibility with all sterilization methods, and unmatched tolerance to chemicals and cleaners used in healthcare facilities. See Medical Grade PEEK.
- Radel PPSU (polyphenylsulfone) is recognized for its ability to retain physical properties after multiple sterilization cycles in all standard methods. Its spectrum of custom healthcare colors has led to applications in short term surgical trials and handles for different instruments in surgical kits. See Radel 5500 PPSU.
- Udel PSU (polysulfone) withstands repeated sterilization in a number of systems and has the benefit of transparency with a light yellow tint in natural form. It also has good mechanical rigidity and toughness. See Udel 1700 PSU.
- Ultem HU 1000 PEI (polyetherimide) was developed as a medical grade of Ultem PEI for short-term contact. It has the high strength, sterilization resistance and toughness inherent in the standard grades of Ultem PEI. See Ultem HU 1000 PEI.
- Ultem HU 1004 PEI is a proprietary polymer blend based on polyetherimide that meets the requirements for devices in contact with bodily tissue and fluids for up to 29 days. The material withstands repeated sterilization with minimal effect on properties and colors. See Ultem HU 1004 PEI.
- Ixef PARA (polyarylamide) offers a smooth surface finish plus the rigidity of a glass-reinforced polymer for instruments and other applications that see single or limited sterilization cycles. Genesis has unique technology for converting the polymer into extrudable shapes and injection molded parts.
Injection molding compared with machining
Genesis customers move to injection molding as a step up from machining when quantity requirements for a medical grade thermoplastic component grow. Tooling cost can be significant, but higher unit volumes usually justify the investment, with tooling amortized over the design life of the component.
Beyond tooling economics, molding changes the per part cost structure. It offers substantial savings in both material and operator hours compared with machining a part from a stock shape such as a rod or plate. Complex features that require multiple setups in machining can often be formed in a single molding operation.
Where volumes do not yet justify tooling, precision machining from stock shapes remains the right route, and Genesis supplies both.
Near Net Shapes
Near net shapes serve as a cost effective transition between machining and full production tooling. The technique uses low cost tooling to mold approximate-dimension parts or blanks that are then finish-machined to exact tolerances. It reduces the material removed in secondary machining and can be a cost-effective manufacturing step until volumes require committing to the cost of a full production mold.
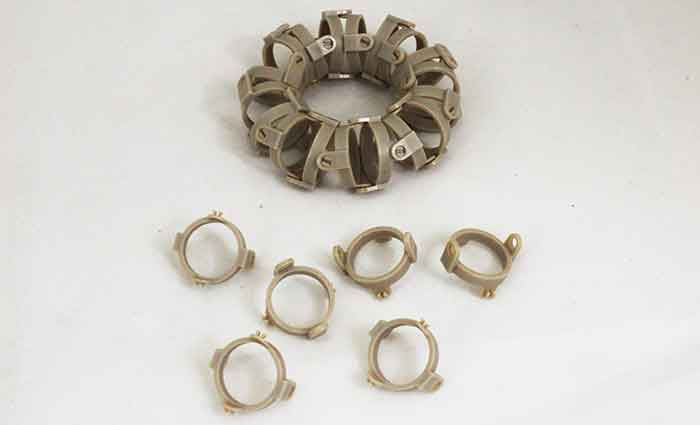
The molding process at Genesis
Material drying
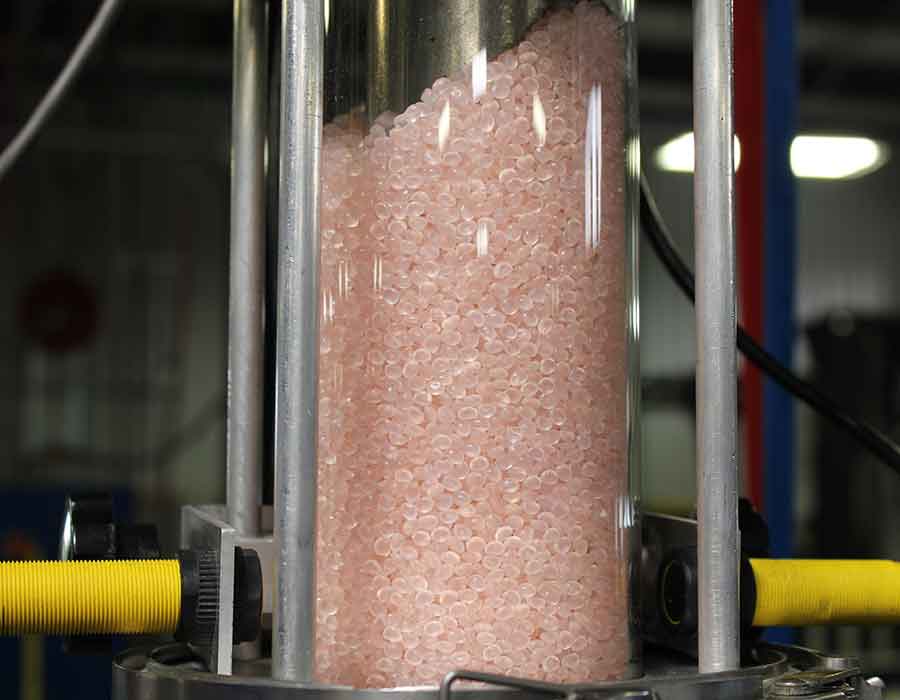
Before molding, the thermoplastic is pre dried in pelletized form. This removes moisture that can create appearance and performance problems in the molded component. Dedicated dryers are used so that material is not cross contaminated between jobs.
Melt and injection
Pellets are melted in the barrel of the molding machine with temperatures controlled to prevent heat degradation of the polymer. Molten polymer is injected under pressure into the mold cavity, where it takes on the dimensions and design features of the component.
Cooling and ejection
The component solidifies during cooling and is ejected from the mold. Cycle time, cooling profile and ejection are set during process development and then held under in mold process control.
Equipment and process control
Genesis uses all electric injection molding machines. These machines use no hydraulic systems, which eliminates the risk of hydraulic fluid leakage as a contamination source in a medical component.
Machine Tonnages and Equipment Capabilities
Designed by the company’s process engineers, Genesis’ injection molding machines are sized and built to process a comprehensive range of medical polymers, part configurations and unit volumes. Capabilities include:
- Machine tonnages: 35, 55, 200, 300, 750
- Injection-compression technology for void-free thick section molding
- Micro-molding machine
- Versatile shot size capability: 0.85 to 570 grams
Process Controls
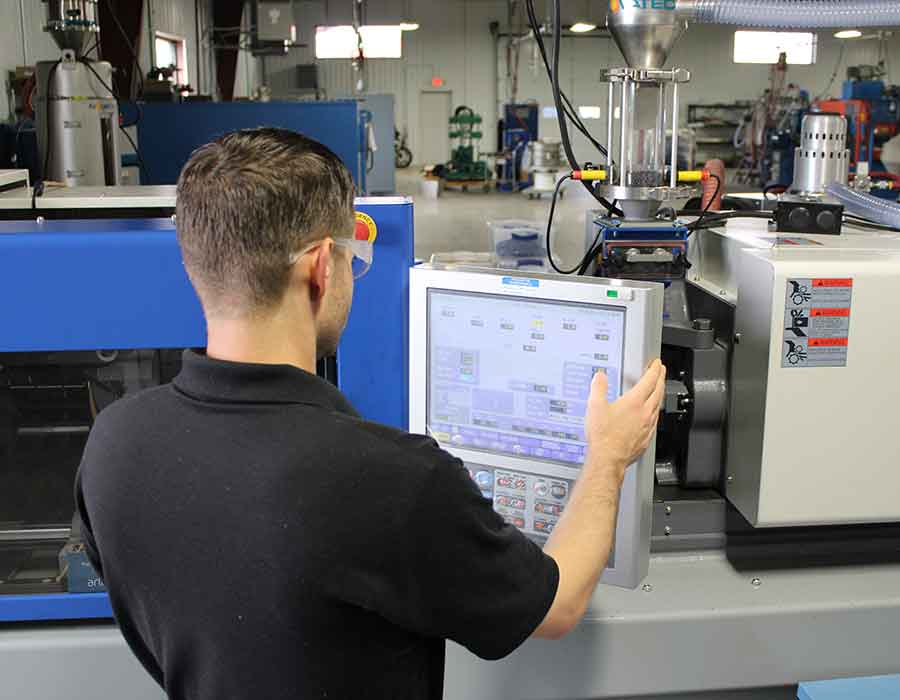
Genesis’ process control systems instantaneously adjust conditions as needed to hold optimum process conditions throughout the molding cycle for each polymer and grade.
In-cavity pressure monitoring maintains pressures at the correct level within the mold itself, and RJG process controls monitor and maintain ideal melt temperatures and pressures in the machine barrel.
Post-processing procedures document the repeatability and quality consistency across a production campaign.
Production tooling
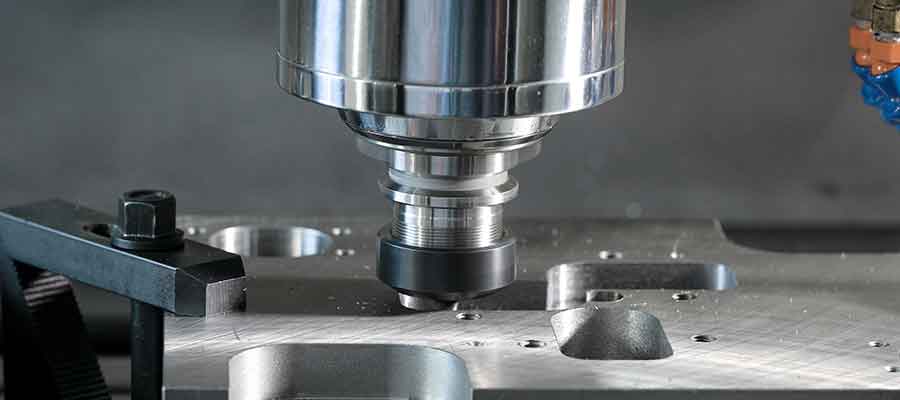
Mold design drives part quality, cycle time and cost. Genesis provides mold building and maintenance services, and sees mold design as a key step in optimizing process development for a device project rather than as a separate exercise handed to a third party.
Tool Transfers
There are instances when an injection molder can no longer continue to produce parts for an MDM. Genesis has the in-house capabilities to accept existing production tooling transferred by MDMs, then upgrade, recondition or modify it as needed so it can return to full operational production on Genesis molding machines.
Quality system, standards and compliance
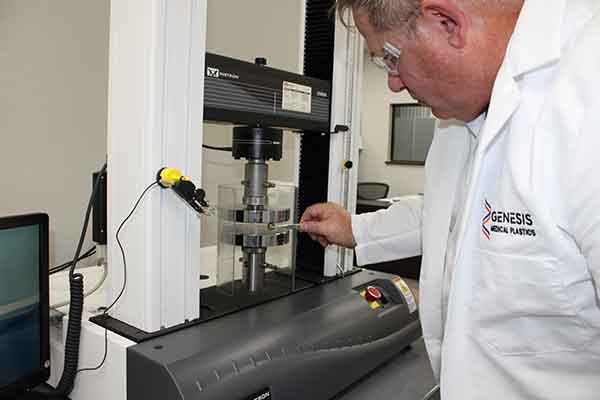
Genesis operates an ISO 13485:2016 and ISO 9001:2015 certified quality system and is FDA registered as a device manufacturing site. Process validations are performed as IQ, OQ and PQ. While MDMs have the ultimate responsibility for their device’s regulatory approvals, Genesis’ quality systems, manufacturing practices and process engineers support customers as product projects move forward. See quality and regulatory for the certifications as published.
Quality Initiatives
Genesis incorporates several practices into its production protocol that go beyond the requisite steps in quality management:
- Certified Master Molder status for process engineers
- Scientific Molding practices
- Dedicated resin dryers avoid cross-contamination with other materials
- Full tear-down and cleaning of all equipment components after each run to eliminate residue from prior production
- Purge compounds are not used, further eliminating risk of cross-contamination
From prototype to production
Molding is one stage of a part’s life. Genesis supports medical device prototypes in machined form, converts stock shapes for low volume production, and moves the same component into molded production as demand grows. Because the material, the drying history and the quality system do not change across that transition, the process development work done early is not discarded.
Genesis also provides tolling services and contract services for customers who supply their own resin or need a broader scope of manufacturing support.
Applications
Molded components are used across the device categories Genesis serves, including spinal implants, surgical instrumentation, arthroscopy, dental and cardiovascular devices.
Request a quote on a molded component
Send the part drawing, the polymer grade and the annual volume. Genesis engineers will review moldability, tooling approach and the conversion route that fits the volume. Request a Quote or contact our experts.
FAQs: Medical Injection Molding
What materials can Genesis injection mold?
Genesis molds high performance medical thermoplastics including PEEK, polyetherimide and polysulfone grades, and molds the polymers customers supply or specify. The grades Genesis converts are listed on the materials pages.
What shot size range do Genesis' machines cover?
Shot sizes per molding cycle run from 0.85 to 570 grams, on machines from 35 to 750 tons, plus a micro-molding machine.
Why all electric molding machines for medical components?
All electric machines use no hydraulic systems, which removes hydraulic fluid leakage as a contamination path in a medical component.
At what volume does injection molding become more economical than machining?
It depends on part geometry, material cost and the design life over which tooling is amortized. Genesis reviews the part and the annual volume and recommends the conversion route rather than applying a fixed threshold.
Can Genesis injection mold implantable grade PEEK?
Genesis converts implantable PEEK resin from major suppliers, or from MDMs on a tolling basis, into injection molded parts. Confirm the specific grade and material form required for your application with Genesis engineering.
Are parts molded from ASTM F2026 compliant implantable PEEK resin also compliant with the same standard?
The process variables in injection molding have an impact on a part's residual stresses and dimensional stability, physical properties and crystallinity levels. While using an F2026-compliant PEEK resin helps, MDMs must have injection molded parts tested to verify that they satisfy the mechanical property criteria for implantable PEEK.
Is Genesis implantable PEEK ASTM F2026 compliant?
Genesis PEEK extruded stock shapes, film and resin all meet the requirements of ASTM F2026.